A practical guide to paper-based materials moving from pilot projects into commercial food packaging—and the evidence buyers should request before making an environmental claim.
Recyclable paper is a system, not a surface appearance
A food package is not recyclable simply because the outside looks like paper. Plastic film, aluminium, wax, silicone, adhesives, inks, barrier chemistry and food residue can all affect fibre recovery. A credible assessment asks whether the finished pack can be collected in the target market, broken down by a paper mill and screened with an acceptable yield of usable fibre.
- Paper-based, plastic-free, compostable and recyclable describe different attributes
- Evaluate the complete package rather than the paperboard alone
- Match every claim to the collection and recovery route in the destination market
Water-based barriers are replacing heavier laminated structures
Thin aqueous coatings can add grease, moisture and heat-seal performance while using less polymer than conventional extrusion-laminated paper. The newest commercial papers target bakery boxes, dry snacks, takeaway cartons, cupstock and selected chilled-food formats. Coating weight alone does not prove recyclability: the finished structure still needs repulpability data, fibre-yield results and food-contact documentation.
- Use only the barrier level the food and holding time require
- Check sealing, leakage, staining and softening on the finished pack
- Request repulpability results for the printed and converted construction
Fluorine-free grease resistance is becoming the expected baseline
Paper for oily food traditionally relied on several types of grease-resistant treatment. Newer systems aim to deliver oil resistance without intentionally added fluorinated chemistry. For direct food contact, buyers should still confirm the exact coating, intended temperature, contact time and migration documentation rather than relying on a broad fluorine-free statement.
Wet-pressed molded fibre is moving beyond basic trays
Thermoformed fibre can provide smoother surfaces, tighter tolerances and more refined presentation than traditional rough pulp. It can replace some plastic trays and foam inserts in food, gifting and bottle applications. Draft angles, ribs, wall transitions and nesting geometry must be engineered together so that the part releases consistently, holds the product and ships efficiently.
- Prototype with the real product and outer pack
- Test representative moisture, temperature and handling
- Use nestable geometry to reduce empty transport volume
High-barrier paper is expanding into dry-food applications
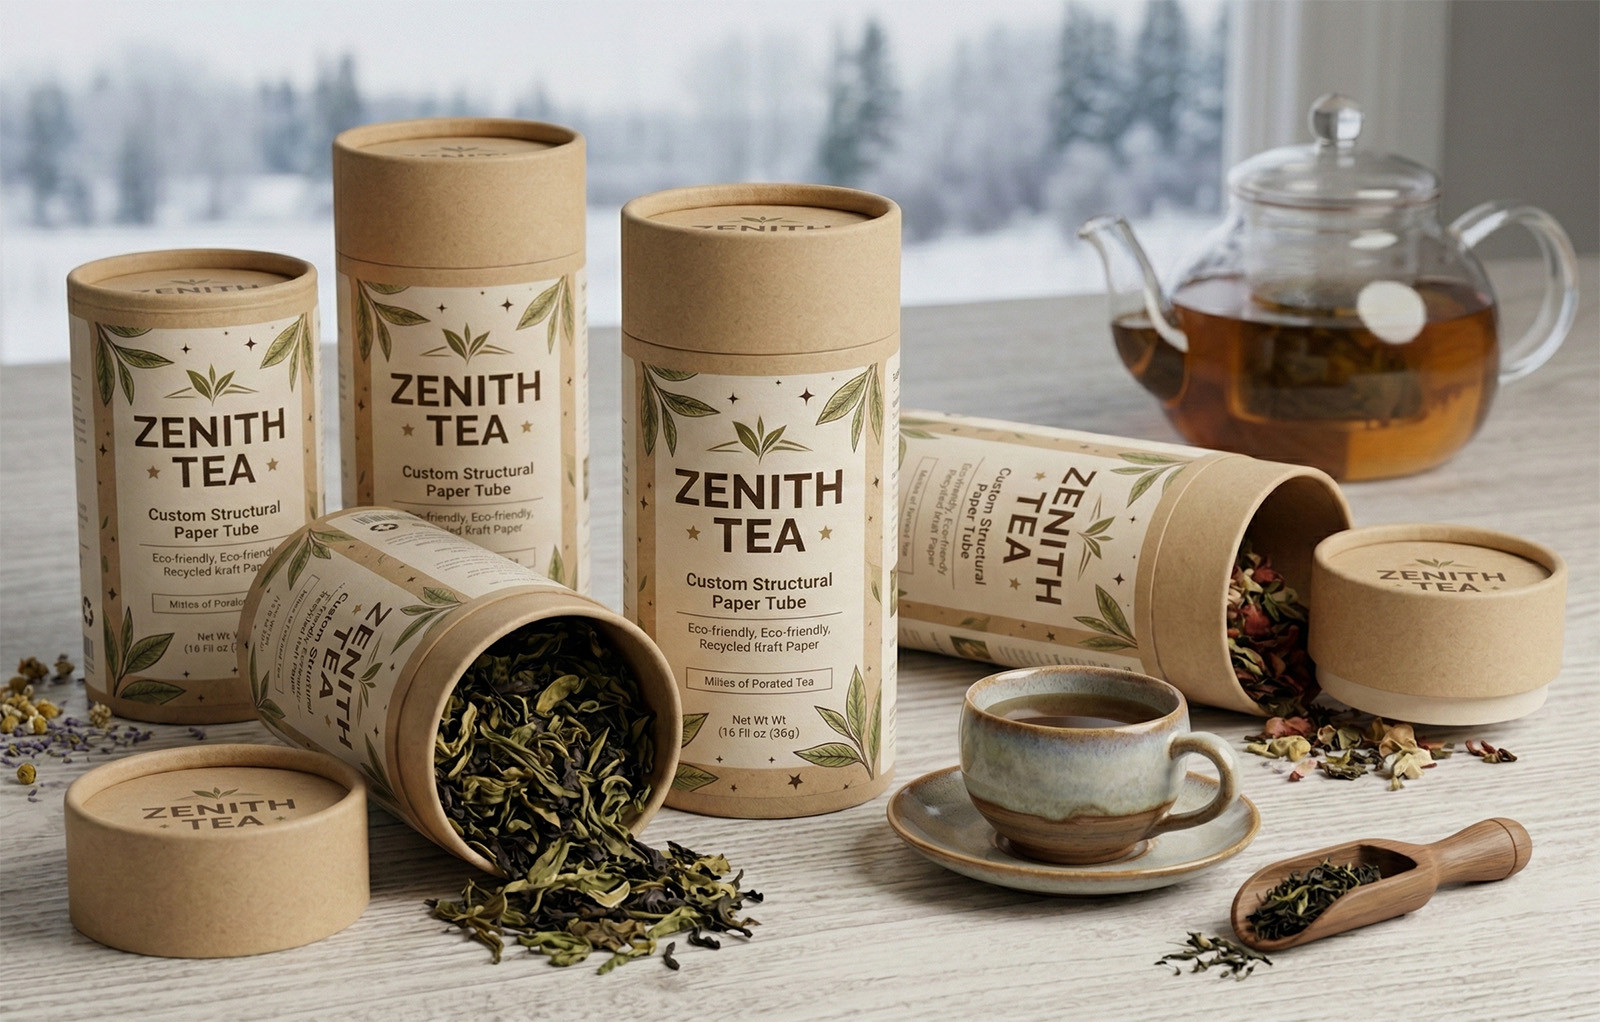
Coated kraft and paperboard structures are improving resistance to water vapour, grease and aroma loss. They are increasingly relevant to tea, confectionery, bakery and selected dry foods. Long shelf-life or oxygen-sensitive products still need application-specific testing; a fibre-based appearance should never substitute for measured shelf-life performance.
Easy separation is the practical bridge to mono-paper
Not every application can become mono-paper immediately. A strong intermediate design uses a paper outer structure with a removable food-contact tray, window or liner. Tabs, friction fits, paper closures and molded-fibre holders can replace permanent plastic inserts, magnets and foam. Components should be easy to identify and separate without tools.
- Keep paper, plastic and metal components mechanically separable
- Avoid bonding a small incompatible component permanently to a large fibre body
- Print clear disposal instructions for each component
The next phase will be evidence-led and application-specific
The market is moving away from broad biodegradable or eco-friendly language toward recovery evidence. Expect lighter and more precisely applied coatings, barrier performance tailored to each food, digital engineering for thinner molded-fibre parts, clearer separation instructions and closer review of adhesives and inks. Food-contact safety and recyclability will increasingly be evaluated together rather than as separate decisions.
- Repulpability method, fibre yield and reject percentage will matter more
- Material declarations will be tied to the approved substrate and converter
- Export projects will need both origin-market and destination-market compliance reviews
A buyer's checklist before approving the material
Start with the product, not the environmental slogan. Define the food, contact conditions, shelf-life target and route to market before choosing a paper. Then validate the finished, converted package through representative physical and documentation checks.
- Food profile: dry, oily, acidic, frozen, hot-filled or reheated
- Contact: direct or indirect, temperature and duration
- Performance: moisture, oxygen, grease, aroma, seal and leakage
- Evidence: food-contact declaration, migration testing and repulpability results
- Recovery: local acceptance, separation steps and consumer instructions